
Introduction
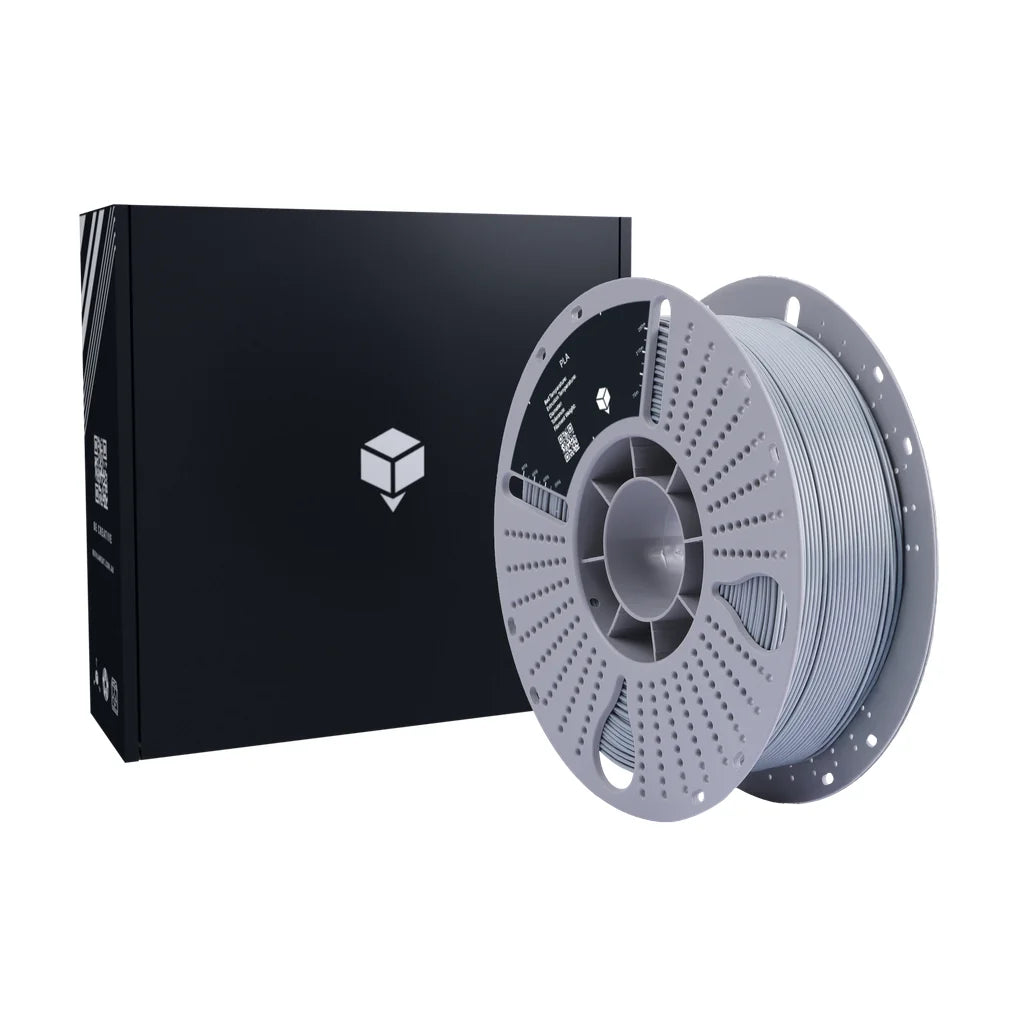
When you are sourcing asa filament australia makers know all too well that our local climate pushes 3D printed parts to their absolute limits. The blistering sun, harsh UV index, and high summer temperatures quickly take a toll on standard hobby plastics, leaving outdoor brackets and fittings brittle, warped, or faded after just a few months in the open.
ASA (Acrylonitrile Styrene Acrylate) has become the go-to technical filament for tackling these exact conditions. Engineered with built-in UV stability, weather resistance, and high thermal endurance, it delivers the functional impact strength of ABS without breaking down under constant solar exposure.
Getting the best out of ASA does require a bit of extra preparation. Because it shrinks as it cools and emits styrene fumes during extrusion, managing warping, bed adhesion, and room airflow is essential for reliable, long-lasting prints.
Table of Contents
- Why Choose ASA Filament in Australia for Outdoor Builds
- Managing Enclosures, Temperatures, and Warping
- Ventilation, Safety, and Moisture Management
- Upgrading to ASA-CF and Post-Processing Finishes
- Frequently Asked Questions
- Conclusion
Why Choose ASA Filament in Australia for Outdoor Builds
Leaving 3D printed parts outside in Australia puts materials to a serious test. Between intense UV levels and high summer temperatures, standard plastics often degrade much faster than expected.
Beating the Australian Sun
The primary reason to run ASA filament for outdoor brackets, antenna mounts, and garden fittings is its built-in UV stabilization. While many common filaments succumb to solar radiation over time, ASA handles continuous sun exposure without yellowing or undergoing brittle degradation.
Materials like PETG offer decent weather resistance, but they can still soften in hot vehicles or lose strength under prolonged exposure. ASA retains its impact strength, colour, and mechanical rigidity even when mounted on a roof rack or an exposed exterior wall.
ASA vs ABS for Outdoor Functional Parts
Chemically, ASA is closely related to traditional ABS filament, offering the same mechanical toughness and thermal resilience makers rely on. However, standard ABS lacks protection against ultraviolet light.
When deciding between the two for a functional build, consider where the part will live:
- ABS for internal applications: Ideal for machinery components, enclosed electronics boxes, and indoor functional parts where direct sunlight is not a factor.
- ASA for exterior builds: The better option for automotive exterior trim, outdoor sensor housings, and weather-exposed fittings that need long-term durability.
Without UV inhibitors, standard ABS oxidises in the sun, leading to faded colour, micro-cracks, and sudden failure under load. ASA preserves the tough mechanical properties and heat tolerance of ABS while resisting solar damage, making it the practical pick for exterior Australian projects.
Managing Enclosures, Temperatures, and Warping
Chamber Heat and Draft Protection
Printing with ASA requires consistent thermal stability. Extruder temperatures should sit between 240°C and 270°C, paired with a heated bed running between 90°C and 110°C. Trapping this warmth inside an enclosed chamber maintaining 40°C to 60°C is vital to prevent layer splitting.
Aussie workshops and garages are prone to sudden temperature shifts. Even a faint gust of wind from an open roller door creates rapid local cooling, shrinking the plastic unevenly and lifting corners mid-print. Keeping the build volume properly sealed keeps ambient warmth steady from the first layer to the last.

Bed Surfaces, Adhesives, and Brims
Smooth or textured PEI build plates offer excellent hold, provided the surface is clean. Applying a light layer of glue stick or liquid adhesive acts as both a bonding agent and an essential release barrier. For demanding jobs using ASA Black or ASA White, a few slicer adjustments make a massive difference:
- Run initial speeds between 40 and 60 mm/s to bed down the first layer.
- Add a wide brim (5–10 mm) to anchor sharp corners on broad footprints.
- Allow the bed to cool fully before removing parts to prevent base warping.
Part Cooling Fan Limits
Excessive airflow is the enemy of layer adhesion with technical styrenics. For standard geometries, keep your part cooling fan turned off completely, or restrict it to a conservative 0% to 20% limit for tight overhangs. Blasting cold air onto newly laid tracks cools the material too quickly, ruining inter-layer bonding and pulling your model apart.
Ventilation, Safety, and Moisture Management
Handling Styrene Fumes Safely
Printing with ASA demands respect for your indoor air quality. Heating the material releases pungent fumes that contain styrene, which can quickly overwhelm an unventilated workshop or hobby room.
You should never run ASA in your living areas without a solid extraction plan. To keep your printing space safe, set up one of the following setups:
- Position the printer in a dedicated, well-ventilated workshop or garage with open windows or active exhaust fans.
- Use an enclosure fitted with active carbon and HEPA filtration to trap both ultra-fine particles and volatile organic compounds.
- Vent the enclosure exhaust directly outside via a duct and an inline fan.
Keeping the enclosure sealed during the entire print helps maintain internal chamber heat while giving your carbon filter time to capture the fumes before you open the door.
Drying and Storing Your Spools
ASA is prone to absorbing ambient moisture from the air, especially in humid Australian regions. Damp filament turns into steam at the hotend, leading to crackling noises, rough surface finishes, and poor inter-layer bonding that weakens functional parts.
To stop this, dry your spool in a filament dehydrator at 80°C for 5 to 8 hours before starting any critical or long build. Once the drying cycle finishes, feed the filament directly from a heated dry box or store it immediately in an airtight container with plenty of fresh desiccant.
For a complete breakdown on keeping your materials dry between projects, check out our guide on how to store 3D printer filament for optimal print quality. Proper storage ensures your ASA delivers the clean extrusion without popping needed for heavy-duty outdoor parts.
Upgrading to ASA-CF and Post-Processing Finishes
Why Print with ASA-CF
If you want outdoor durability with even fewer printing headaches, step up to carbon-fibre-reinforced ASA. Infusing chopped carbon strands into the polymer matrix noticeably changes how the material behaves on the bed. You will find standard spools across our carbon fibre range, including our dedicated ASA-CF Black filament.
Adding carbon fibres delivers several clear practical advantages for functional makers:
- Reduced warping tendencies: The fibres lower internal thermal shrinkage as the print cools, helping sharp corners stay glued to the build plate.
- Enhanced dimensional stability: Parts resist flexing under load and maintain strict tolerances for mechanical assemblies.
- Stunning surface finish: The matte, textured look hides layer lines exceptionally well straight off the printer.
Keep in mind that carbon strands turn filament abrasive. You will need to fit a hardened steel nozzle before running a job, as standard brass will erode rapidly and ruin your extrusion consistency.
Acetone Smoothing and Assembly
Standard ASA reacts to solvents just like ABS, which opens up fantastic finishing options. You can use acetone to transform printed components into seamless, professional hardware.
For exterior parts, vapour smoothing with acetone melts the surface layer slightly, creating a smooth, glossy finish that hides layer stepping entirely. This is particularly handy if you need to wipe away water traps on outdoor sensors or automotive brackets.
Acetone also works as a powerful chemical weld. Brushing a small amount of liquid acetone along a joint chemically fuses the mating faces together. This creates robust, watertight seams that are often stronger than using standard adhesives, making it simple to build assemblies larger than your build volume.
Frequently Asked Questions
Why should I use ASA instead of PLA or PETG for outdoor prints in Australia?
ASA features inherent UV stabilization that keeps it from yellowing or becoming brittle under intense Australian sun exposure. It also handles significantly higher ambient temperatures than standard PLA and PETG, preventing outdoor brackets and vehicle parts from warping or softening in summer heat.
Do I absolutely need a fully enclosed 3D printer to print ASA?
An enclosure is strongly recommended because it traps chamber heat between 40°C and 60°C while shielding the print from ambient room drafts. Without an enclosure, uneven cooling causes rapid thermal shrinkage, resulting in lifted corners and severe layer cracking.
What is the ideal bed temperature to prevent ASA from lifting?
Keep your heated bed set between 90°C and 110°C to ensure strong first-layer adhesion. Pairing this temperature with a clean smooth or textured PEI sheet and a suitable adhesive layer will keep large footprints firmly anchored.
How do I stop ASA prints from delaminating or cracking mid-print?
Prevent delamination by keeping your part cooling fan completely off or restricted to 0% to 20%, maintaining steady warmth in an enclosed chamber, and running moderate print speeds between 40 and 60 mm/s. Making sure your spool is thoroughly dried before printing also protects inter-layer strength.
Does standard ASA require a hardened steel nozzle?
Standard, neat ASA is non-abrasive and prints cleanly with standard brass nozzles without causing premature wear. However, if you switch to composite variants like ASA-CF, you must install a hardened steel nozzle to resist the abrasive chopped carbon fibres.
How should I store my ASA filament when it is not in use?
Keep your ASA spools sealed in airtight storage tubs with fresh desiccant to prevent them from drawing moisture out of the air. If a spool has been sitting out in a humid workshop, dry it in a dehydrator at 80°C for 5 to 8 hours before printing.
Conclusion
Mastering ASA comes down to keeping your thermal environment stable, dialling in your bed adhesion, and setting up proper ventilation for styrene fumes. While it demands a bit more care than standard materials, the payoff is exceptional weather resistance and mechanical toughness that easily stands up to the harsh Australian elements.
Whether you need neat spools for smooth finishes or carbon-fibre-reinforced blends for rigid mechanical brackets, Blue Ember has you covered. Browse the full Blue Ember filament range to find the right materials for your next outdoor build.