
Introduction
When printing complex overhangs, deep cavities, or intricate moving assemblies on a dual-extrusion machine, standard breakaway supports often leave frustrating scars and rough marks. Using pva filament solves this problem completely by acting as a sacrificial scaffolding that washes away entirely in plain tap water, leaving behind smooth, blemish-free surfaces.
Because PVA bonds seamlessly with your build material and dissolves cleanly, you can set interface gaps to zero for flawless bridges and crisp underhangs. However, getting reliable results requires understanding how the polymer behaves. Australian humidity, tricky bed adhesion, and hotend cooking can quickly cause headaches if your setup isn't dialled in correctly.
With a few practical storage habits and the right slicer settings, you can eliminate nozzle jams and enjoy hassle-free dissolvable supports on every dual-material project.
Table of Contents
- What is PVA Filament and How Does It Work?
- Handling Moisture Sensitivity and Storage
- Dialling In PVA Filament Extrusion and Bed Adhesion
- Dissolving and Post-Processing Support Geometries
- Frequently Asked Questions
- Conclusion
What is PVA Filament and How Does It Work?
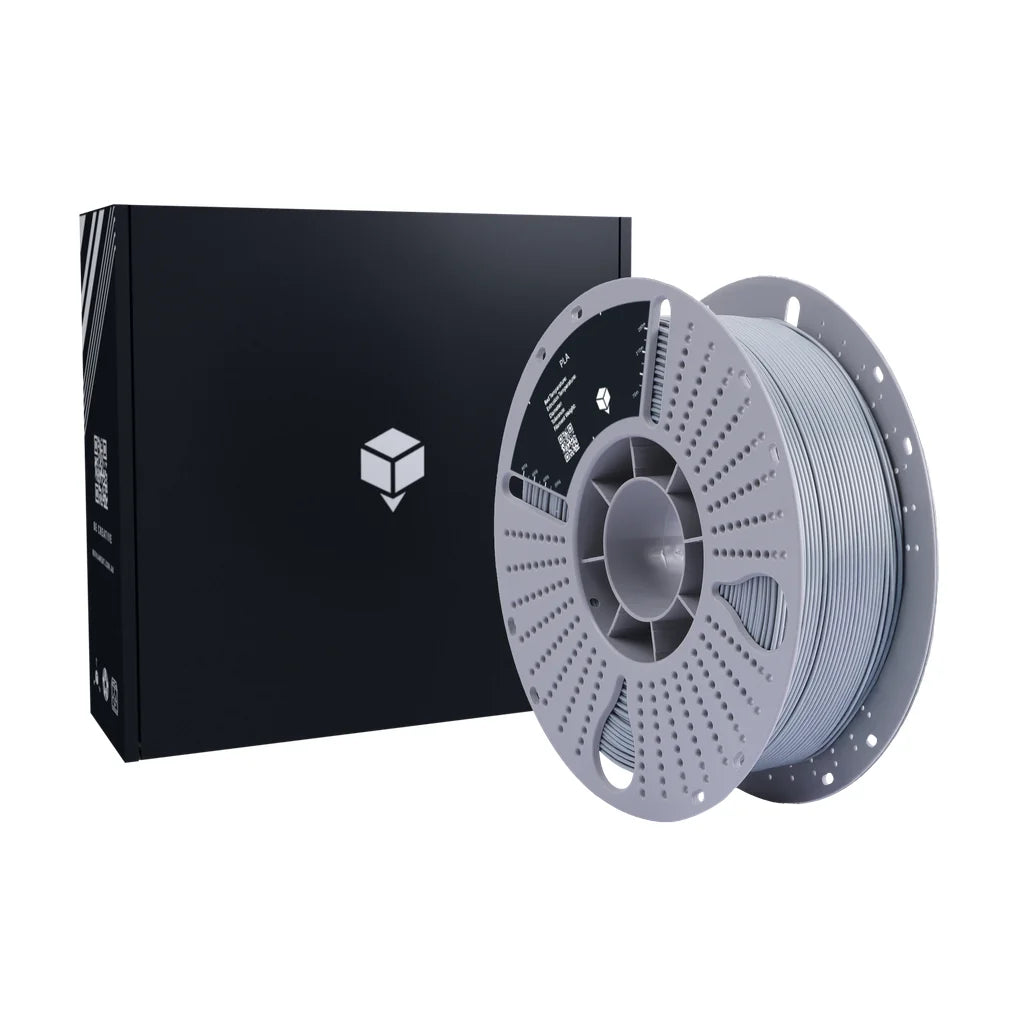
Polyvinyl alcohol, commonly known as PVA, is a synthetic polymer designed specifically to dissolve in ordinary water. Unlike breakaway supports that leave rough scarring or require tricky mechanical trimming, our PVA filament range allows you to print complex internal cavities, overhangs, and moving assemblies without worrying about post-processing tool marks.
Why PVA Pairs Best with PLA
PVA is the classic companion for standard PLA filament in dual-extrusion setups. This combination works exceptionally well because both materials share very similar thermal requirements:
- Overlapping printing temperatures: PVA typically extrudes between 185°C and 215°C, matching standard PLA hotend settings neatly and preventing heat creep issues during material swaps.
- Matched bed settings: Both materials stick reliably at heated bed temperatures between 45°C and 60°C, minimising the risk of thermal shock or warping along shared bottom layers.
- Solid cross-adhesion: Because their melt profiles align, the two polymers bond securely while printing, preventing mid-air support failures on steep overhangs.
Configuring Slicer Interfaces for Zero Gap
When using standard breakaway supports, slicers leave an air gap between the support structure and the model so you can actually snap them apart. With water-soluble material, you can turn this gap off entirely.
By setting your top interface spacing to a zero-clearance interface gap, the PVA prints directly flush against the model's underside. This provides total physical support to the molten PLA as it deposits, creating mirror-smooth overhangs and crisp bridges. Once the print finishes, you simply soak the part in water, and the entire contact boundary washes away without leaving any surface blemishes behind.
Handling Moisture Sensitivity and Storage
PVA is designed to dissolve in water, which means it will pull moisture straight out of the surrounding air at an aggressive rate. In an Australian workshop or shed, especially during humid coastal summers, an exposed spool can take on enough atmospheric water to cause problems in just a few hours. Keeping your PVA Natural spool dry is the single most important habit for reliable dual-extrusion printing.
Signs of Wet PVA
When damp PVA hits a hot nozzle, that trapped water boils instantly. Look out for these telltale warnings:
- Popping, hissing, or crackling noises at the hotend during extrusion.
- Swollen filament that binds, slips, or jams in the extruder drive gears.
- A foamy, inconsistent bead leaving visible gaps and weak support structures.
- Excessive oozing and stringing across your build plate.
Drying and Storing Your Spool
If your filament has taken on moisture, don't write it off. You can restore it using a dedicated filament dryer, a food dehydrator, or a convection oven set to 45°C to 50°C for 6 to 10 hours. Keep a close eye on the temperature to ensure you do not soften the spool or cause the strands to stick together.
Because PVA degrades quickly when exposed to humidity, never leave it sitting on an open spool holder between jobs. Transfer it straight from the printer into an airtight dry box with fresh silica gel or calcium chloride desiccant packs. For detailed setups and protective container options, read our guide on how to store 3D printer filament for optimal print quality to keep your spools running smoothly print after print.
Dialling In PVA Filament Extrusion and Bed Adhesion
Running PVA alongside your primary build material requires balancing temperatures so both materials deposit cleanly without cross-contamination. PVA prints reliably with a hotend set between 185°C and 215°C, making it an ideal companion when pairing with our range of PLA filaments. A heated bed temperature between 45°C and 60°C provides the warmth needed to keep supports stable across longer multi-material print jobs.
Preventing Hotend Carbonisation
Unlike standard thermoplastics, PVA is exceptionally heat-sensitive and will cook quickly if kept under heat without flowing. Leaving PVA sitting inside a heated nozzle leads to thermal degradation and clogs as the material crystallises and hardens against the internal bore.
- Purge idle nozzles: Configure standby temperatures in your slicer so the inactive hotend drops in heat while the primary core lays down build material.
- Use a prime tower: Adding a dedicated prime tower or ooze shield ensures fresh material flows smoothly right before the support layer begins, equalising nozzle pressure after tool swaps.
First Layer Anchor Techniques
PVA can be reluctant to grip smooth build surfaces on its own, increasing the risk of early layer peel. Securing a reliable foundation relies on straightforward prep before you hit start:
- Degrease the surface: Wipe the bed thoroughly with isopropyl alcohol to strip away oils and dust that break contact.
- Apply a thin adhesive layer: Spreading standard PVA glue stick across the plate establishes strong first-layer bed adhesion and stops delicate support trees from breaking loose mid-run.
By keeping standby heat low and ensuring the plate is clean, your support scaffolds will remain planted right through the print.
Dissolving and Post-Processing Support Geometries
Water Temperature and Agitation Tips
Dissolving PVA supports works best when you manage your wash bath thoughtfully. Using warm tap water under 40°C dramatically speeds up the dissolution process without risking heat damage or warping to your primary PLA print. Avoid anything hotter, as excess heat can distort your detailed printed features.
Still water quickly becomes saturated right around the support interface, creating a sluggish barrier that slows the breakdown. Introducing gentle water agitation—whether with a small magnetic stirrer, an aquarium pump, or simply stirring the bath occasionally—keeps fresh water moving over the contact surfaces and cuts down total soaking time.

Step-by-Step Dissolution Method
You can clear away supports faster by actively helping the material break down rather than simply letting a heavy block sit submerged for hours:
- Submerge your finished print fully in a clean container filled with warm water.
- Let the print soak for roughly 10 to 20 minutes until the outer layers of the material soften into a gel-like consistency.
- Lift the part out and peel away bulk layers using pliers or your fingers to remove the heaviest accessible support sections.
- Place the print back into the bath to dissolve any remaining traces in tight crevices or internal cavities.
- Finish by giving the part a thorough rinse under running water to clear away residual sticky film, then leave it on a rack to dry completely.
If you are planning your next dual-extrusion build, you can browse our range of materials across the Blue Ember filament collection to pair reliable PVA with your favourite build filaments.
Frequently Asked Questions
What is PVA filament and how does it work?
PVA (polyvinyl alcohol) is a water-soluble thermoplastic used as a temporary support material in multi-material 3D printing. It prints flush against your model's overhangs and completely dissolves when soaked in water, leaving clean contact surfaces with no tool scarring.
Can I use PVA filament with materials other than PLA?
PVA is best suited to PLA because both polymers share matching thermal ranges for hotends and print beds. Higher-temperature materials like ABS or polycarbonate require print temperatures that far exceed PVA's thermal limits, causing the PVA to degrade and cook inside the nozzle.
Why does my PVA filament keep clogging my printer nozzle?
The two main causes of PVA clogs are moisture and idle baking. If the filament is damp, trapped water boils instantly inside the nozzle, while leaving PVA sitting stationary in a hot nozzle causes heat creep and polymer crystallisation that blocks the bore.
How do I fix PVA that won't stick to the print bed?
Start by thoroughly degreasing your build plate using isopropyl alcohol to remove dust and oils. Applying a light, even layer of standard PVA glue stick and running your heated bed between 45°C and 60°C will help anchor the initial support layers firmly.
How long does it take for PVA supports to completely dissolve?
Dissolution can take anywhere from a couple of hours to overnight depending on the bath volume, water movement, and water temperature. You can cut down soak times significantly by pulling the print out after 10 to 20 minutes to peel away bulk, softened support chunks by hand before returning it to the bath.
Is it safe to pour dissolved PVA wastewater down the drain?
Yes, dissolved PVA wash water is safe for disposal via standard municipal sewer systems. Simply pour the water down your sink and run plenty of warm tap water afterwards to flush any thick, concentrated residue completely through household pipes.
Conclusion
Mastering water-soluble supports comes down to a few steady workshop habits: store your spool in an airtight dry box, lower idle hotend temperatures to prevent heat creep, prep your bed with glue stick, and dissolve the finished print in warm, circulating water. Once these fundamentals are locked in, you can print ambitious, highly complex designs without worrying about post-processing tool marks.
When you are ready to tackle your next detailed dual-material model, load up with Blue Ember PVA for dependable overhangs and easy clean-up. Browse the full Blue Ember filament range to find the ideal match for your 3D printer.